
- Site Navigation -
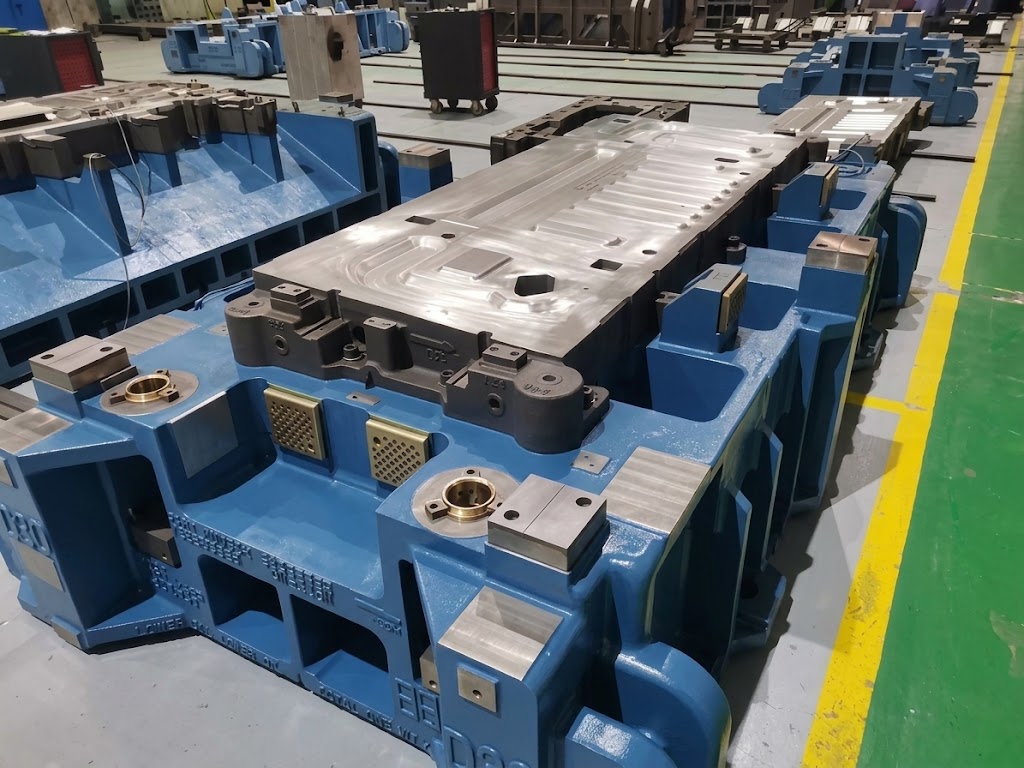
How can I prevent wrinkling defects in my stamping die production?
Date: 2026-09-21 10:59:50 Author: Haoxinran Views: 101 times
How can I prevent wrinkling defects in my stamping die production?
Wrinkling represents one of the most common and challenging defects in sheet metal stamping production, affecting part quality, dimensional accuracy, and downstream assembly operations. Understanding the root causes of wrinkling and implementing effective prevention strategies is essential for maintaining production quality. This FAQ provides comprehensive guidance on wrinkling prevention in stamping operations.
Understanding Wrinkling Defects
Wrinkling appears as wavy folds or creases in the material surface, typically occurring in unsupported areas of the stamped component. The defect originates from compressive stress states that cause material buckling. Wrinkling most commonly appears in:
Flange areas during deep drawing operations
Vertical walls of deep drawn components
Blank holder regions with insufficient pressure
Large flat areas with inadequate support
Primary Causes of Wrinkling
Several factors contribute to wrinkling formation:
Insufficient blank holder force allowing material buckling
Excessive material influx rates into the die cavity
Low material stiffness due to thin sheet thickness
Non-uniform material flow across the component
Poor lubrication causing uneven friction conditions
Improper blank shape design
Prevention Strategies
1. Blank Holder Force Optimization
Proper blank holder force represents the first line of defense against wrinkling:
Apply sufficient force to prevent material buckling
Distribute force uniformly across the flange surface
Use variable force profiles for complex geometries
Implement zone-based force control for challenging areas
2. Draw Bead Implementation
Draw beads effectively control material flow and prevent wrinkling:
Strategically place draw beads in critical flow areas
Optimize bead geometry for desired flow restriction
Use multiple beads for more complex flow control requirements
Balance flow restriction to prevent both wrinkling and tearing
3. Material Flow Control
Controlling material flow patterns prevents wrinkling:
Optimize blank shape for uniform material distribution
Use lubrication strategically to manage friction
Adjust draw radii to influence material flow rates
Use CAE simulation to predict and optimize flow patterns
4. Die Design Modifications
Several die design features help prevent wrinkling:
Increase draw radii to reduce stress concentrations
Add support ribs or pads in critical areas
Optimize binder surface geometry
Incorporate intermediate forming operations for complex geometries
Process Monitoring and Control
Effective production monitoring helps maintain consistent results:
Regular inspection for early wrinkle detection
Blank holder force calibration verification
Lubrication consistency monitoring
Material batch quality control
Statistical process control tracking defect rates
Troubleshooting Wrinkling Issues
When wrinkles appear during production, follow this systematic approach:
Identify wrinkle location and characteristics
Determine if wrinkling is consistent or random
Check blank holder force settings and condition
Inspect draw bead condition and geometry
Verify material properties and lubrication conditions
Make incremental adjustments and evaluate results
Frequently Asked Questions
Q: Does material thickness affect wrinkling tendency?
A: Yes, thinner materials wrinkle more easily because they have less resistance to buckling. Thicker materials require relatively lower blank holder forces for equivalent wrinkling prevention.
Q: Can wrinkling be completely eliminated?
A: With proper die design and process optimization, wrinkling can be effectively controlled within acceptable quality limits. Complete elimination may not always be practical for very complex geometries.
Q: How does material type influence wrinkling?
A: Material properties like yield strength and elastic modulus influence buckling resistance. Higher strength materials generally wrinkle less easily than softer materials under equivalent conditions.
Conclusion
Preventing wrinkling defects requires combination of proper die design, optimized process parameters, and rigorous production monitoring. By understanding the mechanisms that cause wrinkling and implementing appropriate prevention strategies, manufacturers can maintain consistent quality and minimize production losses.
References
Sheet Metal Defect Prevention Guidelines - Manufacturing Standards
Wrinkling Control in Deep Drawing - Engineering Research Publications
Material Flow Optimization - Manufacturing Technology Research
Contact Us
- Company Name: Hebei Haoxinran Machinery Manufacturing Co.,Ltd.
- Hotline: +86 18932785670
- Email: project@haoranmj.com
- Website: https://www.hxrmetal.com
- Address: Across from Sanjing Distillery on Road 4, Botou Economic Development Zone, Cangzhou City, Hebei Province
Copyright © 2026-2027 https://www.hxrmetal.com. All Rights Reserved. Hebei Haoxinran Machinery Manufacturing Co.,Ltd.