
Surface Treatment and Coating for Stamping Die Longevity: Matching the Fix to the Failure
Date: 2026-11-01 04:43:11 Author: Haoxinran Views: 100 times
A stamping die fails at its surface long before the bulk steel gives out. Galling, adhesive wear, and chipping start where the tool meets the sheet, and that is exactly where surface treatment earns its keep. At Haoxinran we specify coatings based on which failure mode a given section faces, because one treatment does not fit every die face.
Where Dies Actually Wear Out
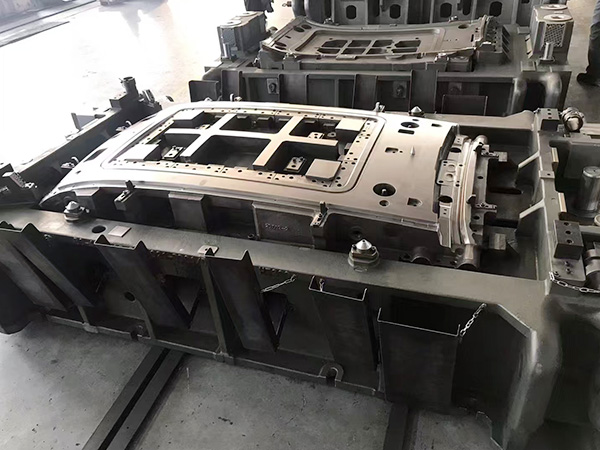
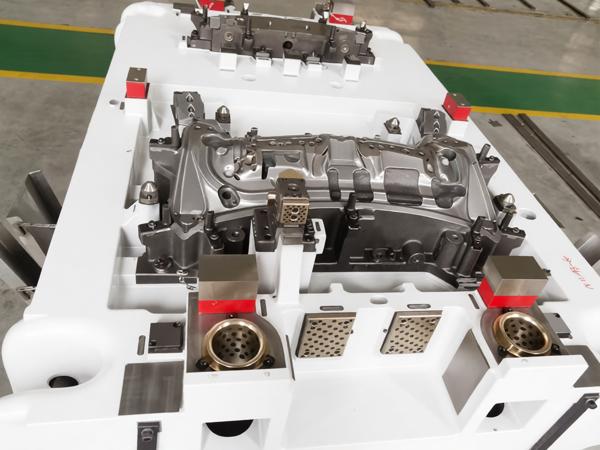
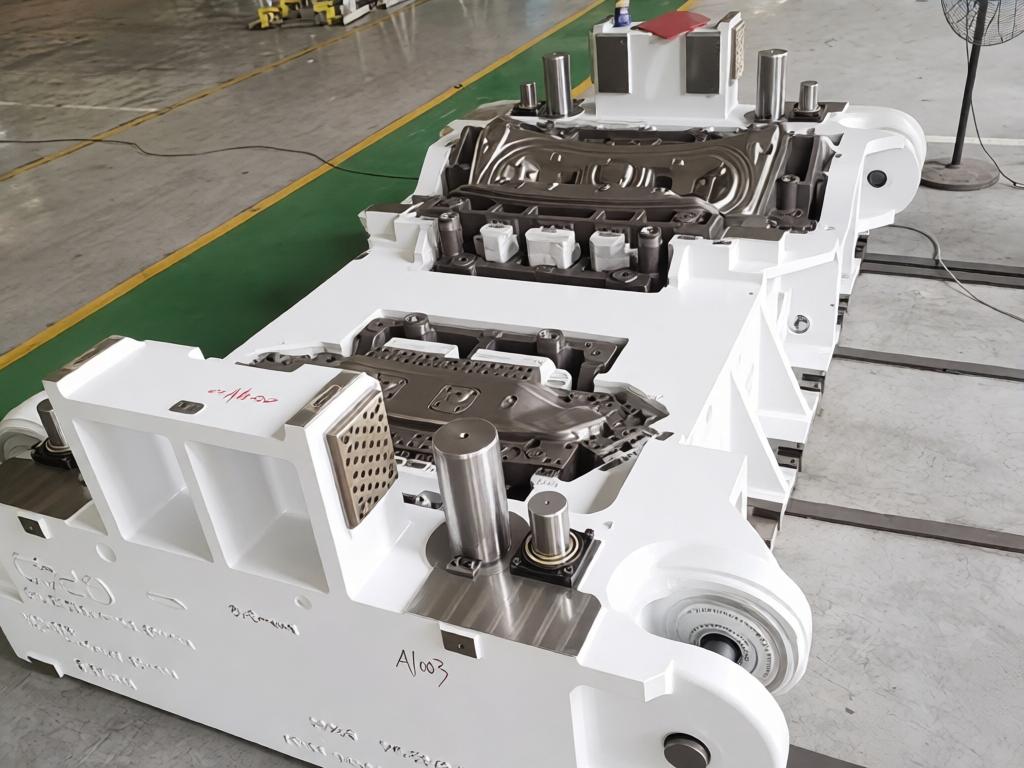
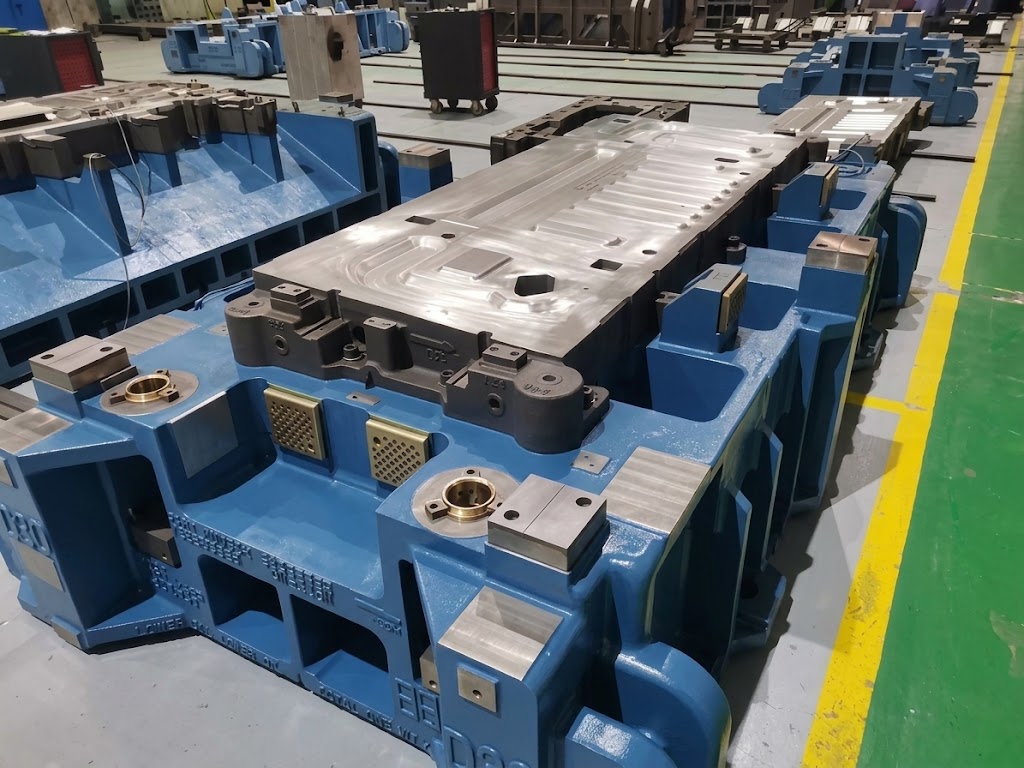
The forming surfaces and the trim edges are the two trouble zones. Forming faces gall when soft sheet sticks and tears away tool material; trim edges wear and chip from the cutting action. The right coating lowers friction on the former and hardens the latter. Picking by symptom, not by habit, is the discipline that extends die life.
Nitriding for the Baseline
Nitriding diffuses nitrogen into the surface to make a thin, hard case without changing the bulk. It is cheap, stable, and a good default for draw and form faces that mostly need lower friction and mild wear resistance. The case is thin, so it does not help much where heavy impact chips the edge, but for sliding contact it is hard to beat on cost.
TD Coating for Severe Wear
Thermal diffusion, often called TD coating, grows a vanadium carbide layer on the tool that is extraordinarily hard and resists galling even against high-strength steel. It is the go-to for trim and pierce sections that see the worst abuse. The process runs hot and can distort thin inserts, so it is planned during design, not added after a failure.
PVD and Thin Films
Physical vapor deposition puts a thin, smooth film, such as titanium nitride, on the surface with little heat and almost no distortion. It is ideal for finished or precision sections where distortion is unacceptable. The film is thin, so it suits moderate loads and helps release and corrosion more than it resists heavy abrasion.
Hard Chrome Plating
Chrome plating is the older option: a thick, smooth, corrosion-resistant layer that also lowers friction. It helps on draw surfaces and where the die sees moisture or mixed materials. It can crack under heavy impact, so it pairs poorly with aggressive trim edges, but for form faces it remains a practical choice.
Choosing by Application
The selection is a map from failure mode to treatment. Sliding wear and galling on form faces: nitriding or chrome. Cutting edges under high-strength steel: TD coating. Precision finished sections that cannot distort: PVD. Few dies use one treatment everywhere; a well-built tool mixes them by station.
Care Between Runs
No coating removes the need for care. Correct lubricant, clean blanks, and prompt attention to the first sign of pickup keep a treated surface working. We document the coating on each section so maintenance replaces like for like, because a mismatched re-coat is a common, avoidable cause of early die failure. A coating that looked right on paper but fails in the first week is usually a sign the failure mode was misread, not that the coating was bad.
Re-Coating and Repair
Coatings wear out, and the question is whether to re-coat or replace the section. Thin treatments like PVD and nitriding are often refreshed in place once the substrate is sound, which is far cheaper than a new insert. TD and chrome, being thicker or hotter processes, are planned more carefully and sometimes mean a new section. The key is to act before the substrate is damaged, because once the base steel wears, no coating restores the geometry that was lost. A section log that records the original treatment and the re-coat dates turns this from guesswork into a schedule, and it prevents the false economy of running a worn face until it fails on a production night.
Cost Versus Life Trade-off
Premium treatments cost more up front but earn it back through fewer stops. On a high-volume line where a die change costs thousands per hour, a TD-coated trim that runs months longer than a nitrided one pays for itself quickly. On a low-volume tool, the same upgrade may never break even. The right call is a life-cost view, not a sticker-price view, and it should be made per section rather than for the whole die, because wear is rarely uniform across a tool and a blanket choice either overspends or underspends somewhere on the face.
References
ASM International, Surface Engineering and Coatings for Tooling
SAE International, Wear Mechanisms in Stamping Dies
Journal of Materials Processing Technology, TD and PVD Coatings for Press Tools
International Organization for Standardization, ISO 9001 Quality Management in Tooling